GEAR MANUFACTURING SOLUTIONS
Industrial Fluids Across the Gear Manufacturing Process
From controlled cooling after forging and gear cutting to heat treatment, grinding, honing and final protection, KERUN provides industrial fluids and application support matched to gear material, module, geometry and process conditions. Our approach supports microstructure control, machining efficiency, dimensional stability and tooth-surface quality.
Gear-Cutting Lubrication & Tool Protection
Gear Quench Distortion Control
Grinding Burn & Tooth-Surface Quality
Low-Residue Cleaning & Rust Protection
GEAR MANUFACTURING
From Gear Blank to Final Delivery
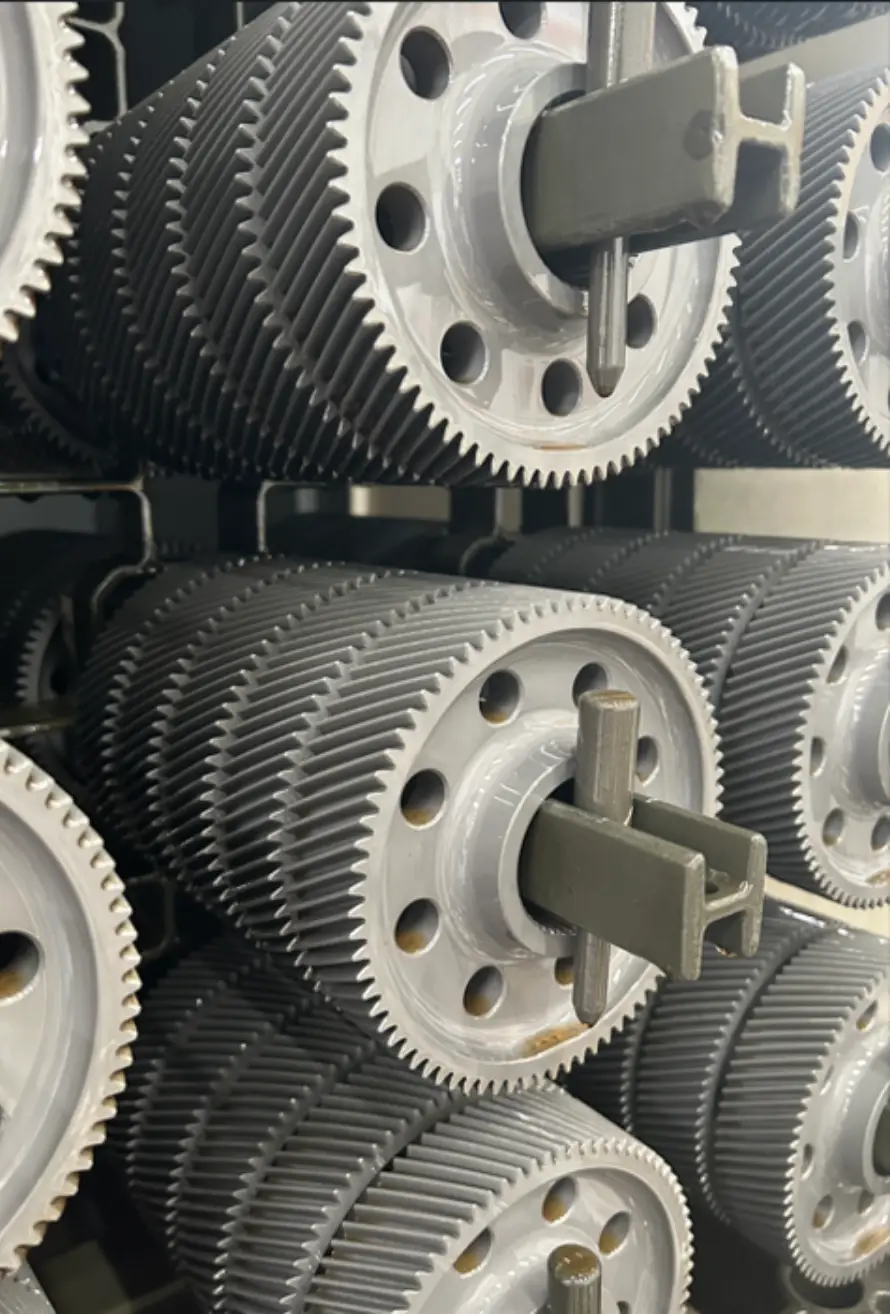
Gear manufacturing combines blank forming, preparatory heat treatment, gear cutting, final heat treatment, precision finishing and protection. These stages influence gear microstructure, accuracy, load-carrying capacity and operating performance.
Typical Manufacturing Process
Normalizing or Controlled Cooling
Rough Machining and Gear Cutting
Heat Treatment
Gear Grinding and Honing
Cleaning, Rust Prevention and Delivery
INDUSTRIAL FLUID APPLICATIONS
Where Industrial Fluids Matter
Industrial fluids perform different roles in microstructure control, gear cutting, heat treatment, precision finishing and final protection. Each stage requires a balance of fluid properties and operating conditions.
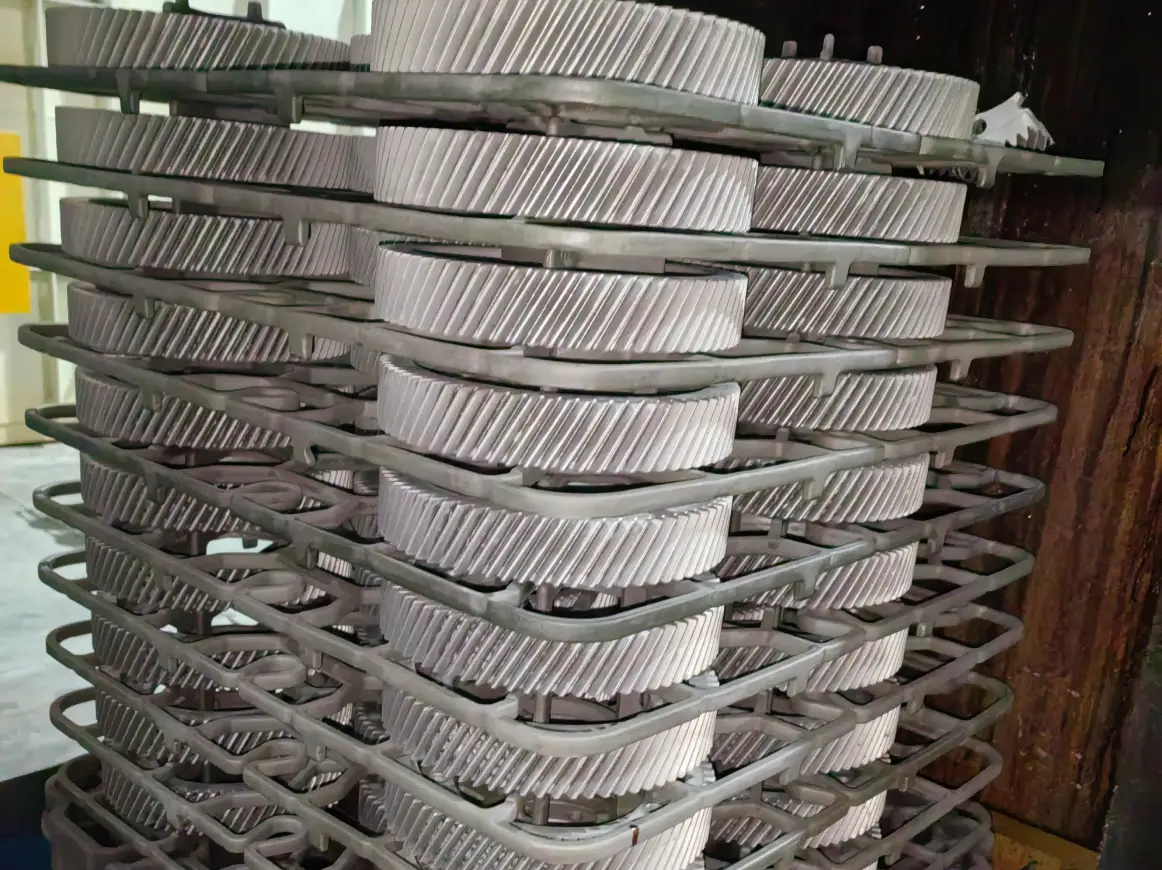
Controlled Cooling After Forging
Uneven cooling of medium and large alloy-steel gear blanks may produce secondary banding, mixed grain structures and granular bainite. Controlling cooling rate and uniformity helps improve microstructure and downstream machinability.
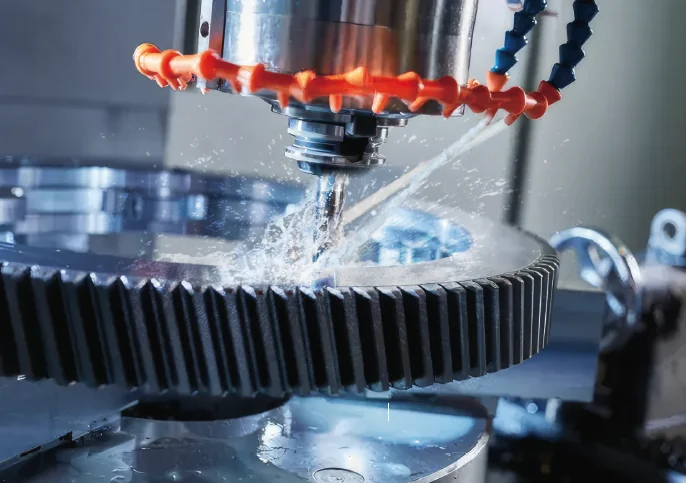
Turning and Gear Cutting
Turning, hobbing, shaping, shaving and gear milling place different demands on lubrication, cooling, chip removal and oil-mist control. Fluid condition and residue can also influence surface finish, tool life and subsequent heat-treatment quality.
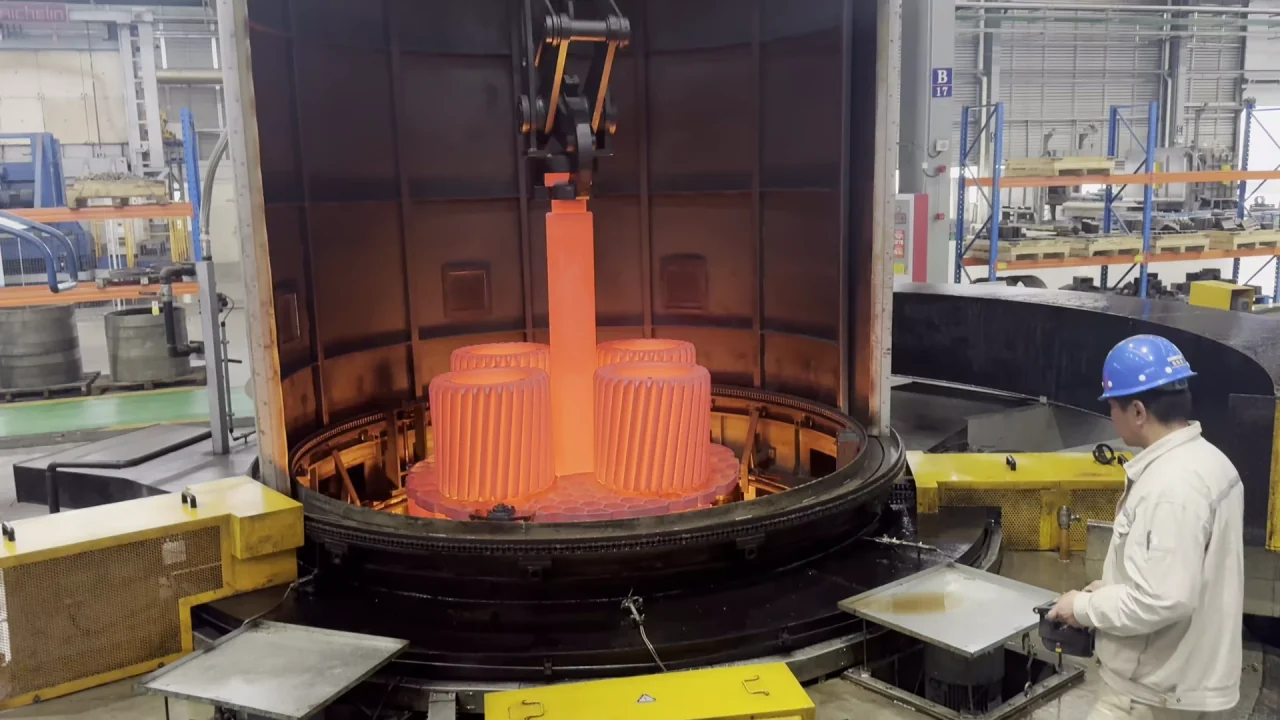
Heat Treatment and Distortion Control
Gear heat treatment may include carburizing or carbonitriding followed by quenching, induction hardening, or quenching and tempering. Material, module, geometry, loading arrangement, cooling rate, fluid temperature and flow uniformity all influence hardness, microstructure and distortion.
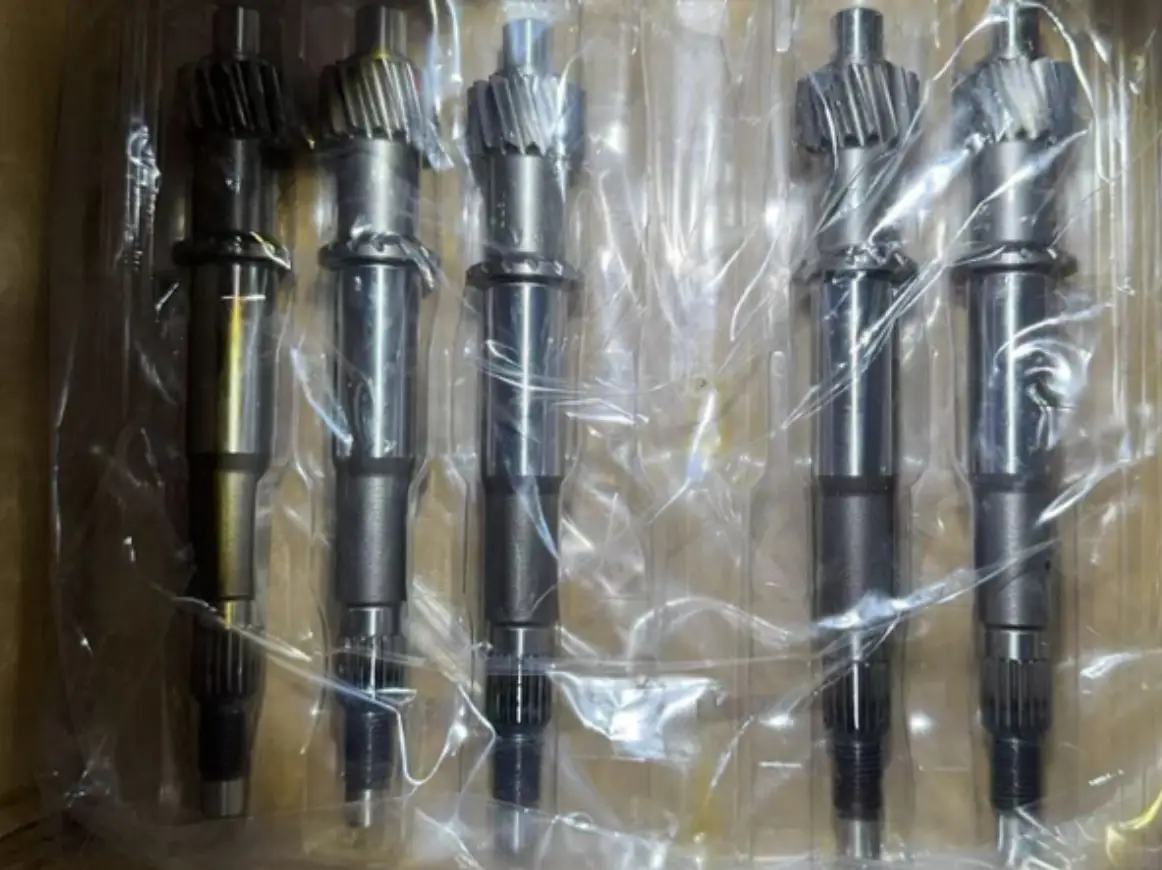
Precision Finishing and Final Protection
Gear grinding and honing improve tooth accuracy and surface condition after heat treatment. Fluid selection needs to balance grinding efficiency, burn control, surface finish and oil mist. Cleaning and rust prevention then protect gears during handling, storage and delivery.
PRACTICAL APPLICATION RESULTS
From Quench Distortion Control to Grinding Burn Reduction
Fluid matching and on-site validation help address gear distortion and grinding burn. The following applications show results achieved for specific components and operating conditions.
Typical Applications
Controlled Cooling of Forged Gear Blanks
Turning & Gear Cutting
Carburizing and Carbonitriding with Quenching
Quenching and Tempering & Induction Hardening
Gear Grinding & Honing
Inter-Process and Final Product Cleaning
Inter-Process and Final Rust Protection
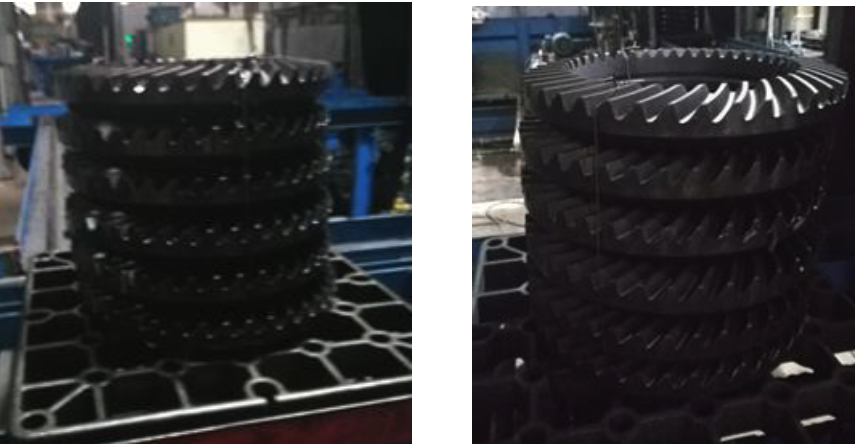
Component
20CrMnTi driven spiral bevel gear; module 10; bore diameter 390 mm.
KR218H Result
Case depth of 1.64 mm and core hardness of 38–40 HRC, with measured warpage controlled under the reported test conditions.
APPLICATION RESULT 01
Distortion Control for a Large-Module Spiral Bevel Gear
A 20CrMnTi driven spiral bevel gear with a module of 10 and a bore diameter of 390 mm required control of case depth, core hardness and quenching distortion. With a customized KR218H formulation, the reported case depth reached 1.64 mm and core hardness reached 38–40 HRC. Inward warpage remained within 0.20 mm for 90% of parts, while outward warpage remained within 0.10 mm for 80% of parts.
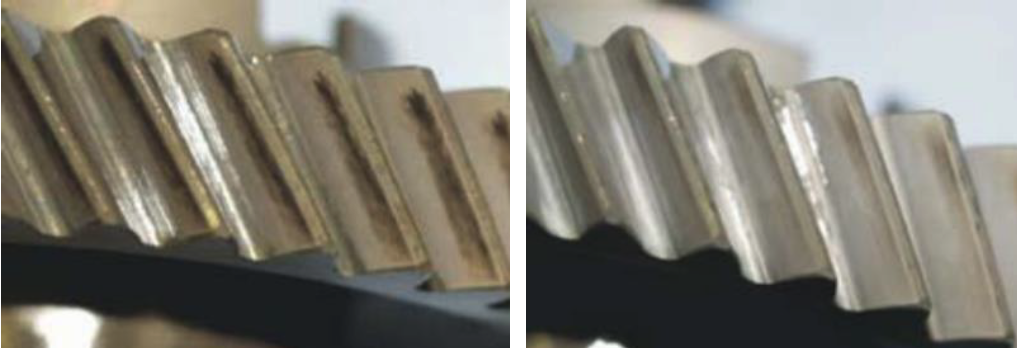
Before
The original application showed tooth-surface grinding burn; the reported wear scar diameter was 0.56 mm.
After
After switching to KR-C10, grinding burn improved and the reported wear scar diameter was 0.44 mm.
APPLICATION RESULT 02
Gear Grinding Burn Improvement
In the supplied gear-grinding application, switching to KR-C10 reduced the reported wear scar diameter from 0.56 mm to 0.44 mm. The application also reported an improvement in tooth-surface grinding burn.
RECOMMENDED PRODUCT SYSTEMS
Product Categories for Gear Manufacturing
Explore fluids for controlled cooling, heat treatment, machining, grinding, cleaning and corrosion protection. Select products according to gear material, geometry, equipment and quality requirements.
Controlled-rate cooling Fluid
View Product SystemPrecise cooling control minimizes distortion and cracking for consistent heat treatment results.
Specialized Quenching Oil
View Product SystemProvides reliable quenching protection for diverse heat treatment applications.
Isothermal Classification Quenching Oil
View Product SystemPrecisely controls cooling to reduce thermal stress and quenching distortion.
Synthetic Cutting Fluid
View Product SystemSuitable for various machining applications, extending tool life while improving efficiency and surface quality.
Grinding oil
View Product SystemLow-wear and highly stable lubrication designed for precision grinding applications.
Metal Cleaning
View Product SystemSuperior cleaning performance ensuring component cleanliness and reliability.Rust Prevention
View Product SystemLong-lasting corrosion protection reduces rust risks and preserves metal component performance during storage and use.
RELATED PROCESS SOLUTIONS
Process Solutions for Gear Manufacturing
KERUN matches industrial fluids to gear material, geometry, accuracy requirements and equipment. Explore support for heat treatment, gear cutting and grinding, cleaning and rust prevention.

Heat Treatment Fluid Solutions
Cooling and quenching solutions for gear blanks and heat-treated gears, with attention to microstructure, hardness and distortion control.

Cutting and Forming Fluid Solutions
Fluids for turning, gear cutting, grinding and honing, selected to support lubrication, machining efficiency and tooth-surface quality.

Surface Treatment and Protection Fluid Solutions
Cleaning and rust-prevention solutions for managing process residues and protecting gears between operations and through delivery.
INDUSTRY PARTNERS
Selected Customers and Partners
KERUN supports gear manufacturers with industrial fluid selection and application guidance based on component requirements and production conditions.
Start with Your Gear and Process Conditions
Share your gear material, module, geometry, equipment and process parameters. Tell us about concerns such as post-forging microstructure, quench distortion, hardness, case depth, grinding burn, cleaning residue or rust protection so our technical team can assess suitable fluid options.