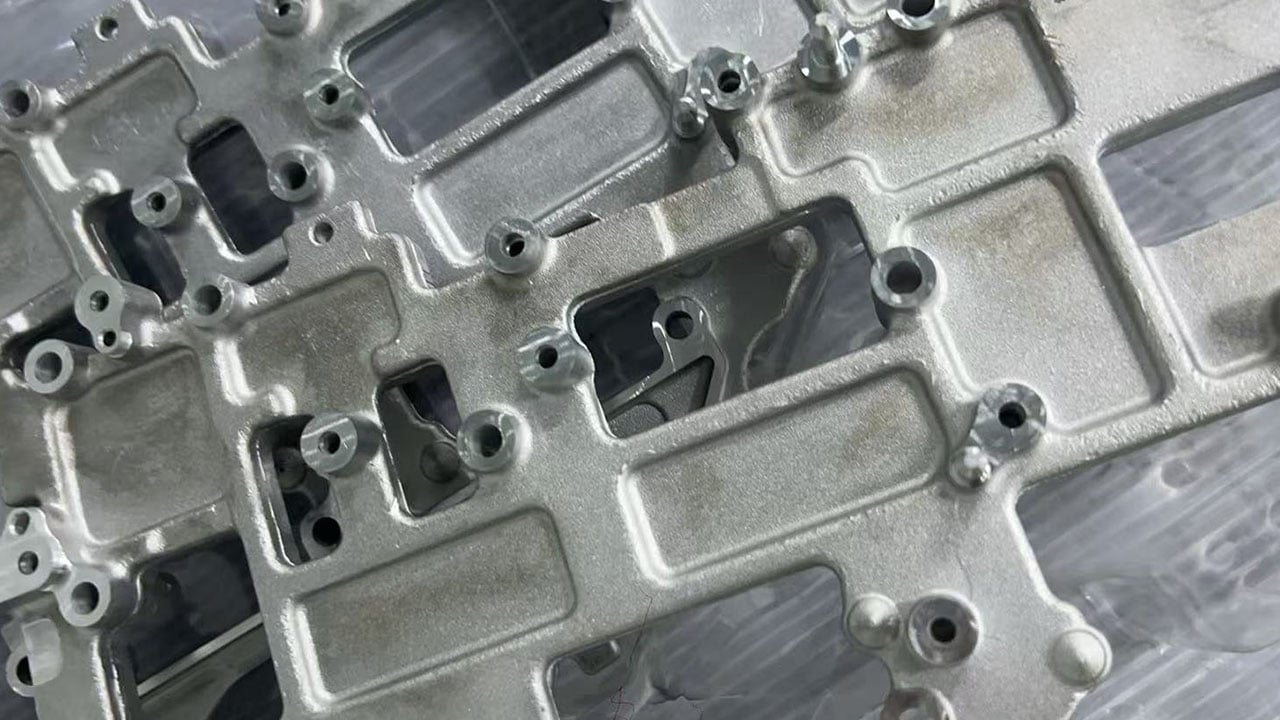
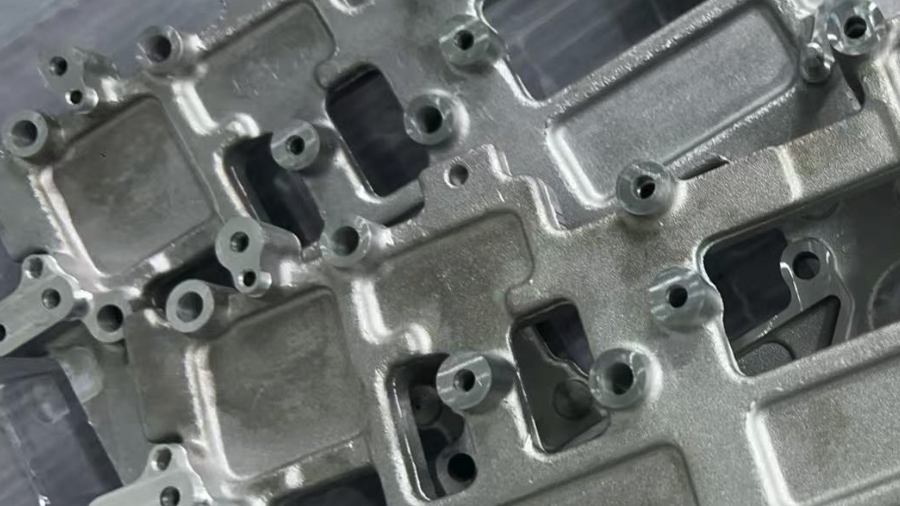
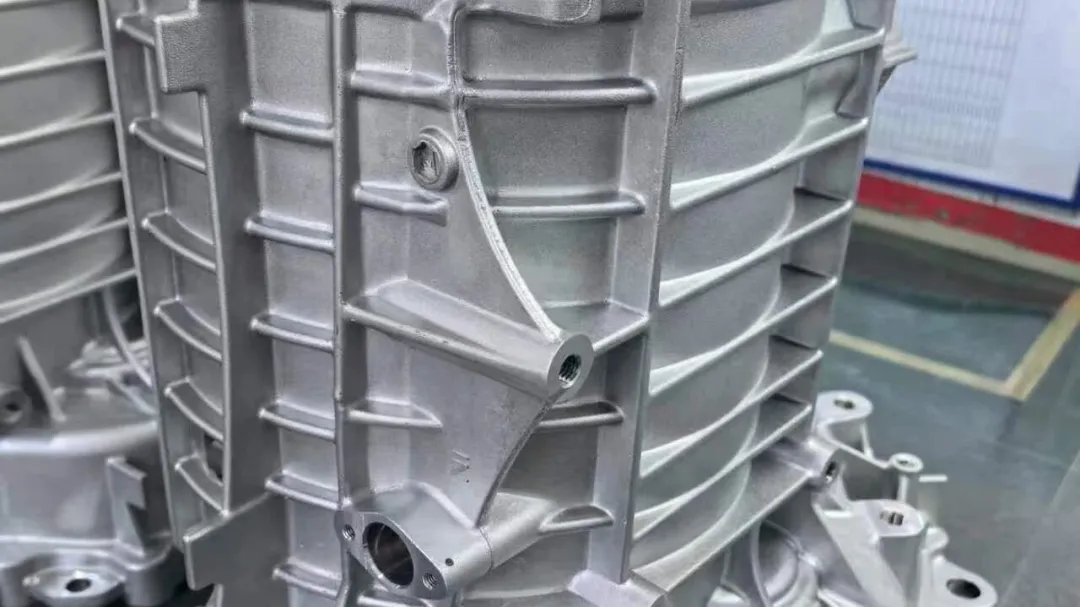
ADC12 aluminum parts may turn dull, gray, or even black after machining. A freshly mixed cutting fluid may perform well, yet surface quality can become less consistent over time—even when fluid concentration and pH remain within the specified ranges.
What causes this change?
Following reports from customers, the KERUN Industrial Fluids Research Institute investigated three questions: what causes corrosion-related staining, how different corrosion inhibitors perform, and how changes in the fluid during use affect surface protection.
The study focused on phosphate ester structure and the ionic environment in water-based cutting fluids, linking laboratory findings to practical troubleshooting.
ADC12 is a widely used die-cast aluminum alloy containing alloying elements such as copper, magnesium, and zinc. Its surface condition can be sensitive to the machining environment.
In water-based cutting fluids, several factors can contribute to discoloration:
Troubleshooting therefore requires a broader assessment of the corrosion inhibitor system, water quality, and operating conditions, alongside concentration and pH.
Phosphate esters are commonly used to inhibit aluminum corrosion in water-based metalworking fluids. Their molecular structure influences how they adsorb onto the metal surface, form a protective film, and withstand changes in the ionic environment.
KERUN evaluated seven phosphate esters with representative molecular structures using full-immersion corrosion tests on ADC12 aluminum specimens.
Table 1. Corrosion ratings of aluminum specimens after immersion in purified-water test solutions.
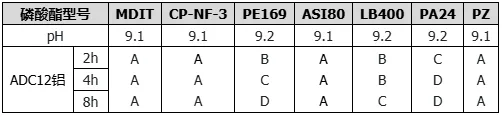
Some branched-chain alkyl phosphate esters formed relatively compact, hydrophobic adsorption films. After eight hours of immersion under purified-water conditions, the specimens retained a relatively good surface appearance. Straight-chain octyl phosphate ester also showed good initial film formation under these conditions.
By comparison, some alkyl polyoxyethylene ether phosphate esters formed less complete films. Their greater hydrophilicity and steric hindrance were associated with increased susceptibility to pitting and staining.
These results indicate that inhibitor selection should consider the specific molecular structure and film-forming ability, as well as the additive type and dosage.
Tests in purified water provide a useful baseline for initial protection, but they do not fully represent a cutting fluid in service.
During machining, makeup water can introduce calcium, magnesium, and chloride ions. Reactive aluminum chips can also contribute to the gradual accumulation of aluminum ions in the fluid. These changes can affect phosphate ester performance and the integrity of the protective film.
To investigate this effect, the researchers tested the seven phosphate esters at different calcium and magnesium hardness levels and aluminum ion concentrations.
Table 2. Corrosion ratings of aluminum specimens after immersion in standardized calcium–magnesium hard-water test solutions.
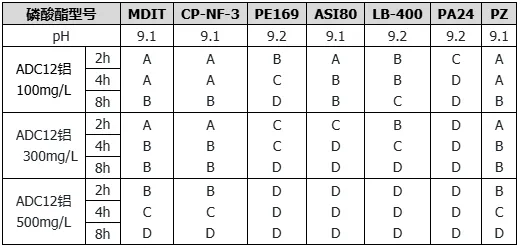
Table 3. Corrosion ratings of aluminum specimens after immersion in test solutions containing aluminum ions.
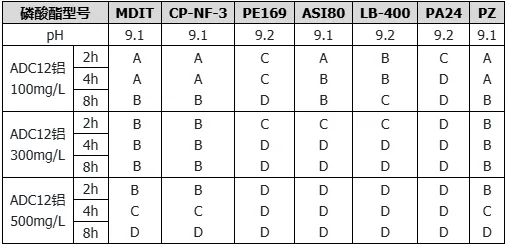
As calcium, magnesium, and aluminum ion concentrations increased, several phosphate esters showed a decline in corrosion inhibition, although the extent varied.
Some branched-chain alkyl phosphate esters were relatively more resistant to these changes and maintained good protection under certain hard-water conditions. Their performance also declined, however, as ion concentrations increased further.
Using purified water for the initial mix does not eliminate this risk. It reduces the introduction of calcium and magnesium ions but cannot prevent aluminum ions from accumulating during machining.
This helps explain why a fluid that performs well when freshly mixed may provide less consistent surface protection after extended use.
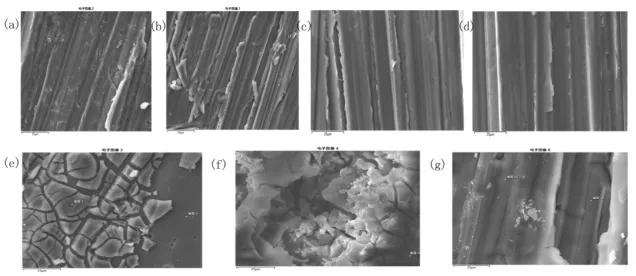
The researchers further examined the aluminum surfaces using electrochemical impedance spectroscopy (EIS), scanning electron microscopy (SEM), and energy-dispersive X-ray spectroscopy (EDS).
The results showed that all the phosphate esters exhibited some adsorption onto the aluminum surface, but the integrity of the resulting films differed considerably.
A compact, continuous film limits direct contact between the alkaline fluid and the aluminum surface, helping reduce corrosion and staining. Gaps in the film leave localized areas exposed, where corrosion can develop into pitting, dullness, or black discoloration.
Figure 1. Nyquist plots for aluminum exposed to different phosphate ester test solutions.
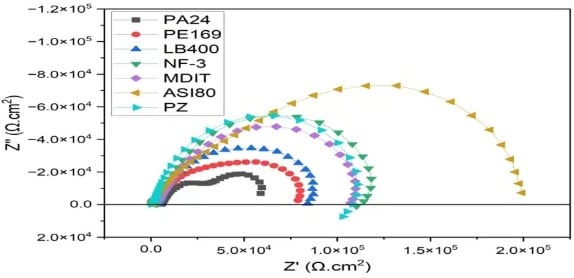
Figure 2. SEM images of aluminum surfaces treated with different phosphate esters: (a) NF-3; (b) MDIT; (c) PZ; (d) ASI80; (e) PA24; (f) PE169; (g) LB400.
Evaluating an aluminum corrosion inhibitor therefore requires more than confirming that it forms a film. The film must also remain effective as water chemistry changes and metal ions accumulate.
The study provides a practical framework for investigating aluminum discoloration:
Simply increasing fluid concentration or adding more corrosion inhibitor may not resolve the underlying issue. Assessing the material, formulation, water chemistry, and operating conditions together provides a stronger basis for identifying the cause and reducing surface defects and batch-to-batch variation.
For KERUN, customer feedback is the starting point for research that supports fluid selection, formulation development, and reliable performance in production. Connecting field observations with laboratory testing and application support helps turn these findings into practical improvements in machining stability and surface quality.


 EN